Production
- Output per day
- Capacity utilisation
- OEE
- Unplanned downtime
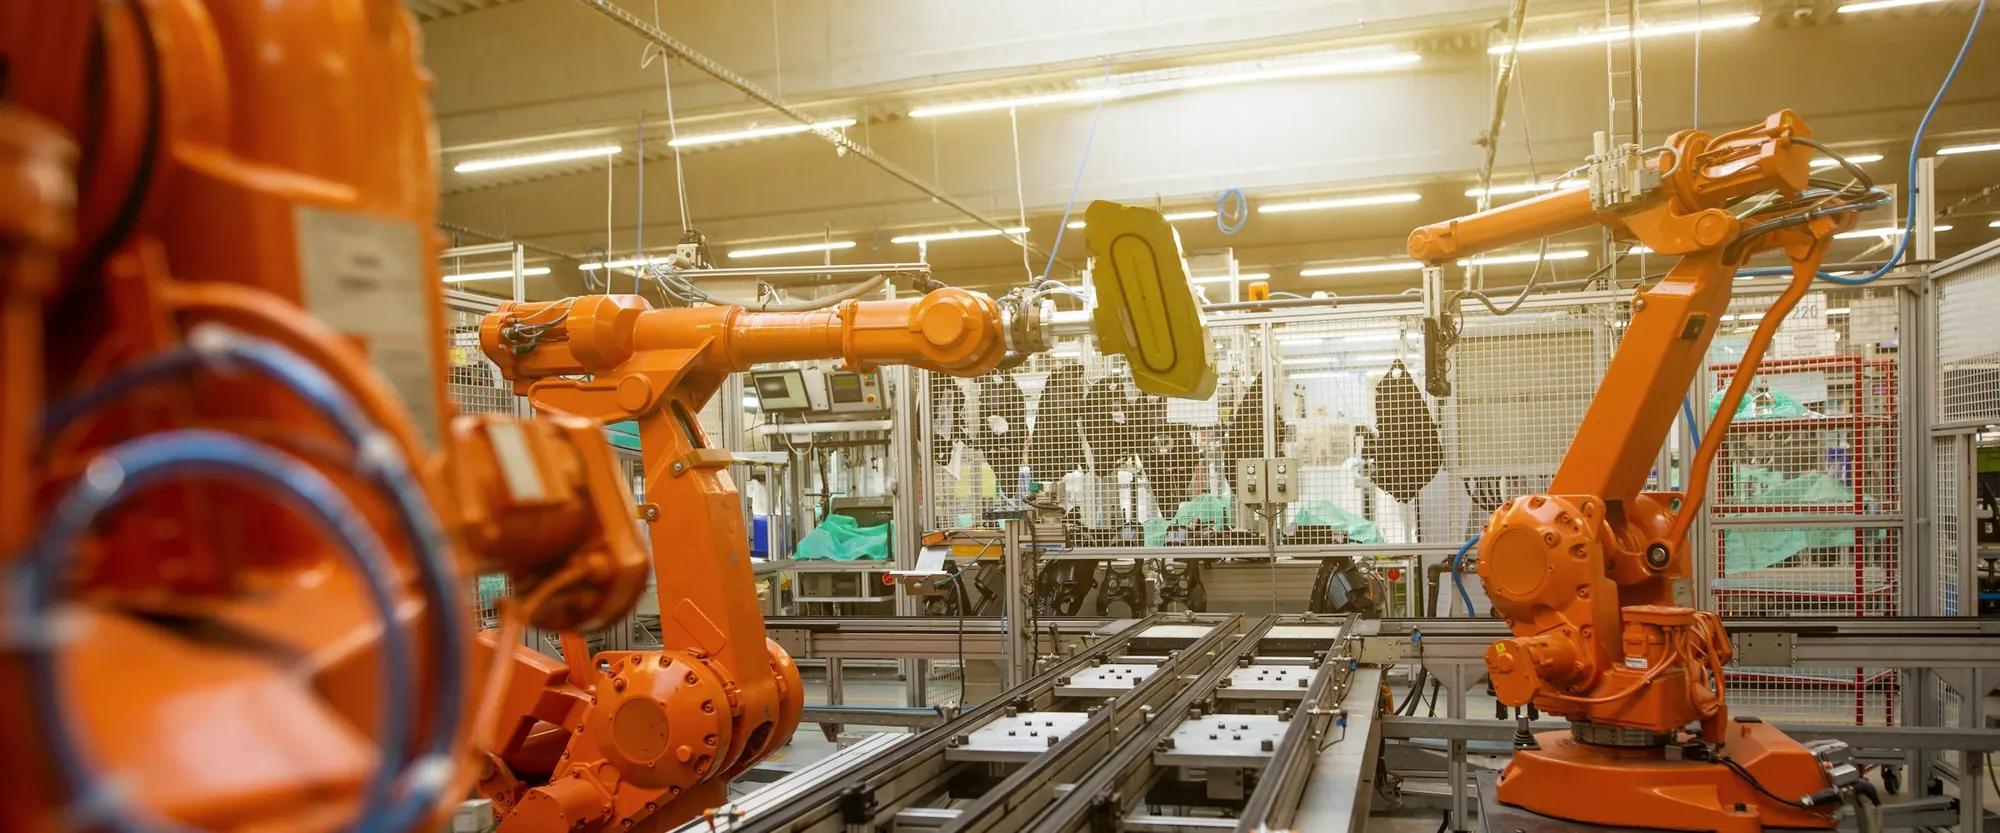
Manufacturing
Manufacturing runs on physical reality — materials, machines, shifts and yield. The recurring technology problem is the delay between what happens on the floor and what the systems believe, and the decisions made in that gap.
Manufacturing ERP & digital core
ERP is the backbone of a manufacturing business — the system where materials, production, quality, maintenance, stock and cost meet. We select, implement, optimise and integrate it, and connect it to the automation, applications and analytics around it.
ERP & business systemsERP platforms we work with
Around the core
Oracle, SAP and Odoo are named as platforms we work with, evaluated on fit. Naming a platform does not imply a partnership, certification or endorsement.
Operating challenges
Most manufacturers do not lack data. They lack timely, trusted data in one place, so planning is defensive and inventory carries the cost of the uncertainty.
Recorded stock and physical stock diverge between counts, so planning adds buffer and working capital absorbs the difference.
Output, scrap and downtime are recorded at end of shift or later, which makes root-cause analysis retrospective.
The real production plan lives outside the ERP, so the system holds a version nobody uses.
Breakdowns are handled as events rather than tracked as a pattern, and the true cost of downtime is not visible.
Actual cost per unit is known after the period closes, which is after the pricing decision was needed.
Transformation opportunities
Stock movements captured where they happen, so planning stops paying for uncertainty.
Output, downtime and scrap recorded close to the event, which turns after-the-fact reporting into a usable signal.
Production and material planning that operations actually use, so the ERP holds the live plan.
Batch and lot traceability designed in, which is a compliance requirement in some segments and a recall control in all of them.
Lead times, order status and supplier performance visible in one place rather than in an inbox.
The manufacturing journey
Each step creates operating data and business transactions. Select a step to see which ones usually matter for planning, costing and service.
Forecasts and orders turned into a production plan.
Operating data
Business transactions
Manufacturing performance dashboard
A conceptual design. Each card shows the kind of measure a connected plant can report — not results from any plant.
01 / 06Production
No figures are shown. Charts are shapes only, not data from any plant or client.
Key business capabilities
Demand, planning, scheduling and production orders.
From requisition to supplier payment.
Work orders, spares and asset history.
Orders, delivery, invoicing and collection.
Inspection, non-conformance and release.
Close, costing and management accounts.
Operational and executive reporting from one source.
Plant systems, warehouse and ERP kept in step.
Typical systems and processes
Transformation options
There is no single roadmap for every manufacturer. These are the three starting points we see most often.
Optimise the systems and processes already in place, with quick, visible wins.
Fits when the platform is sound but under-used.
Add integrated digital tools that close specific gaps and lift efficiency, without replacing the core.
Fits when the data exists but does not connect.
Transform the areas with the highest impact first, in the order the business sets.
Fits when part of the estate has reached its limit.
Why it matters
Why Launch Soft Solutions
If data capture is slower than the line, it will not be done. Interfaces are designed for gloves, noise and speed.
The value is in inventory, planning and costing agreeing with each other, which is integration work as much as ERP work.
Plans account for connectivity, power and workforce availability rather than assuming an idealized plant.
Use cases
Movement capture, cycle counting and the process discipline behind them, so the recorded number can be planned against.
Simple, robust interfaces for operators to record output, downtime and scrap without leaving the line.
Replacing the spreadsheet plan with one the planners prefer, which is the only way adoption holds.
Forward and backward traceability from raw material to dispatch, built for the recall scenario rather than the audit slide.
Asset, failure and intervention history captured so maintenance can move from reactive to planned.
How we deliver
Manufacturing cannot pause for a system. Work is staged around shift patterns, planned maintenance windows and seasonal load, and cutovers are sized to be reversible.
Spend time on the floor and in planning before proposing anything. Documented process and real process differ.
Rank by working-capital impact, downtime cost and how much each blocks the others.
Prove on one line, one product family or one site before extending.
Extend with cutovers timed to production, each one small enough to reverse.
Support and improve under defined ownership, including out-of-hours expectations where shifts require it.
Relevant capabilities
Discovery, selection, implementation, optimization and integration across finance, supply chain and operations — with the platform chosen on fit, never assumed in advance.
APIs, data flows and the continued operation of what has been delivered, under explicit service ownership rather than informal goodwill.
Applications, portals, workflow tools and internal systems built where no packaged product matches how the business actually works.
Assessment, operating-model design and a sequenced roadmap, so modernization is absorbed by the organization rather than announced to it.
Specialised vertical
Kilns, clinker, energy intensity and high-volume dispatch make cement a distinct ERP and integration problem. The cement page covers the production lifecycle, SAP and ERP processes, plant-to-enterprise integration and illustrative dashboards.
One line, one product family or one shift is enough to establish where the delay is and what it costs.